

Phone:
86-15852949220


 |


ALAS
Nanjing, China
L/C, T/T, Paypal, Money Gram
1
Wooden Crate Packaging
| Quantity: | |
|---|---|

For high-mix, small-batch sheet metal fabricators and job shops, frequent tooling changes are the leading cause of machine downtime. The ALAS 4-Way Press Brake Multi-V Die Block is engineered specifically to eliminate this bottleneck. By integrating four distinct, precision-ground V-openings onto a single rotatable alloy steel block, this versatile lower die allows operators to adapt to varying sheet thicknesses in under 20 seconds without a full die replacement.
Unlike massive, single-purpose heavy dies designed solely for thick structural steel plates, this standard 4-way multi-V block is strategically optimized for everyday job shops, maintenance facilities, and rapid prototyping lines. It delivers flawless air-bending performance across a highly versatile thickness spectrum:
Thickness Fluidity: Engineered for seamless processing of conventional sheet metal ranging from 1.0mm to 6.0mm+.
High-Mix Production: Ideal for workshops that constantly cycle through electrical enclosures, cabinets, brackets, and custom architectural hardware.
Prototype Agility: Allows immediate switching between precision thin-gauge sheets and medium structural pieces on a single machine setup.
Traditional setups require operators to physically lift, store, and realign heavy single-V dies whenever a different metal gauge arrives. The ALAS 4-way die completely consolidates your workflow:
60% Setup Reduction: Onsite cases confirm that replacing individual dies with our 4-way rotatable block cuts daily tool-change labor, boosting machine utilization.
Zero-Downtime Rotation: Transitioning between jobs is as simple as releasing hydraulic pressure, cleaning the groove, and rotating the block to your target V-opening.
Space & Cost Consolidation: One single ALAS 4-way die block effectively replaces four individual single-V tools, saving tool procurement budgets and liberating massive amounts of warehouse shelf space.

To ensure long-term structural integrity during multi-spec switching, all ALAS multi-V dies are forged from premium 42CrMo alloy steel (equivalent to AISI 4140). The die undergoes full-body quenching and tempering, combined with precision induction hardening on the V-groove surfaces to reach a balanced hardness of HRC 47±3. This achieves a perfect structural balance: supreme surface wear resistance to prevent galling on stainless steel, backed by high core toughness to resist cracking under eccentric loads.
Performance Features | ALAS Forged 42CrMo Die (Original) | Low-Cost T10 / T10A Alternatives |
|---|---|---|
Hardness (HRC) | 47–52 (V-groove area: 47±3) | 56–60 (High hardness but extremely brittle) |
Tensile Strength (MPa) | 1100+ (High strength, resists fracture) | 1300+ (High strength but low elongation, prone to snapping) |
Heat Treatment Process | Overall quenching & tempering + V-groove induction surface hardening | Conventional overall quenching + low-temperature tempering (Simple & low cost) |
Wear Resistance | Excellent (Supported by Cr-Mo alloy & surface strengthening) | Average (Only for soft sheets, easy scratching on stainless steel) |
Toughness (Crack Resistance) | Excellent (Hardly broken transversely under load) | Poor (Critical defect: easy cracking under impact or eccentric load) |
Service Life | 8–10 years (Standard CNC long-service die, regular regrinding available) | Unpredictable service life (Usable for 1-2 years roughly, sudden failure likely) |
Sourcing Advice: Select ALAS 42CrMo hardened dies for mass production, stainless steel bending, and high-frequency workshop use. Low-cost T10/T10A material is only applicable for low-budget projects and occasional ordinary thin iron sheet bending without mass production. This material features high brittleness and poor pressure resistance, forbidden for stainless steel bending, which may crack under impact force.
For conventional air bending applications, selecting the appropriate V-opening width directly reduces bending resistance and preserves the die's shoulder radius.
The Air Bending Rule: Standard V-opening width (V) = Sheet Thickness (T) × 6 to 8 for thin gauges, and T × 8 to 12 for medium plates. An enlarged, wide V-opening drastically reduces bending pressure and protects the die from premature shoulder wear when processing tougher materials.
Versatile Shop-Ready Layouts: ALAS provides carefully balanced, standard industrial V-opening configurations ground symmetrically into the block cross-section:
Precision Thin Sheet Focus: 6mm, 10mm, 14mm, 20mm
General Fabrication Standard: 16mm, 24mm, 35mm, 50mm (Most Popular)
Operation Reminder: Undersized V-opening selection will cause workpiece cracking and die edge damage. Always keep the V-opening width within the 6×~12× sheet thickness range for safe and precise bending.

ALAS universal 4-way dies feature a standard square base configuration, allowing direct installation onto most conventional hydraulic press brake die holders. Custom shank profiles, specialized base heights, and tailored locating dimensions are precision-machined to fit major equipment brands seamlessly.
Machine Clamping Style | ALAS Tailored Compatibility Solution |
|---|---|
Standard Square Bed / Holder | Direct drop-in installation for universal hydraulic bending machines. |
Amada / Promecam style | Custom lower shanks available (please specify machine model when ordering). |
Trumpf / Wila Clamping | Precision ground to match original equipment quick-clamping dimensions. |
LVD / Durma Adaptations | Customizable base widths and alignment notches to ensure perfect centering. |
Legacy & Non-Standard Brakes | Bespoke die heights and base dimensions machined to match old-style tables. |
Parameters to Confirm Before Ordering: Total die height allowance, lower shank type/width, and your worktable's current clamping mechanism mode.
The maximum load capacity depends on the active V-opening dimension and the raw material core. ALAS 42CrMo hardened dies are built to withstand standard workshop pressures safely. The data below indicates the safe tonnage limit per 1000mm die length for mild steel. We highly recommend reserving a 10%–15% safety load margin for daily onsite operations.
Active V-Opening Width | Max Recommended Tonnage (Per Meter) | Optimal Sheet Thickness Spectrum |
|---|---|---|
16 mm | 25 Tons | 1.5 mm – 2.5 mm |
24 mm | 40 Tons | 2.5 mm – 4.0 mm |
35 mm | 65 Tons | 4.0 mm – 6.0 mm |
50 mm | 120 Tons | 6.0 mm (Maximum limit for standard block) |
Operation Warning:Overload operation is strictly prohibited. Forcing thick, high-strength plates into an undersized V-opening will cause permanent V-groove deformation, edge deformation, or base splitting. A complete rated tonnage validation report is delivered with every ALAS tooling shipment.
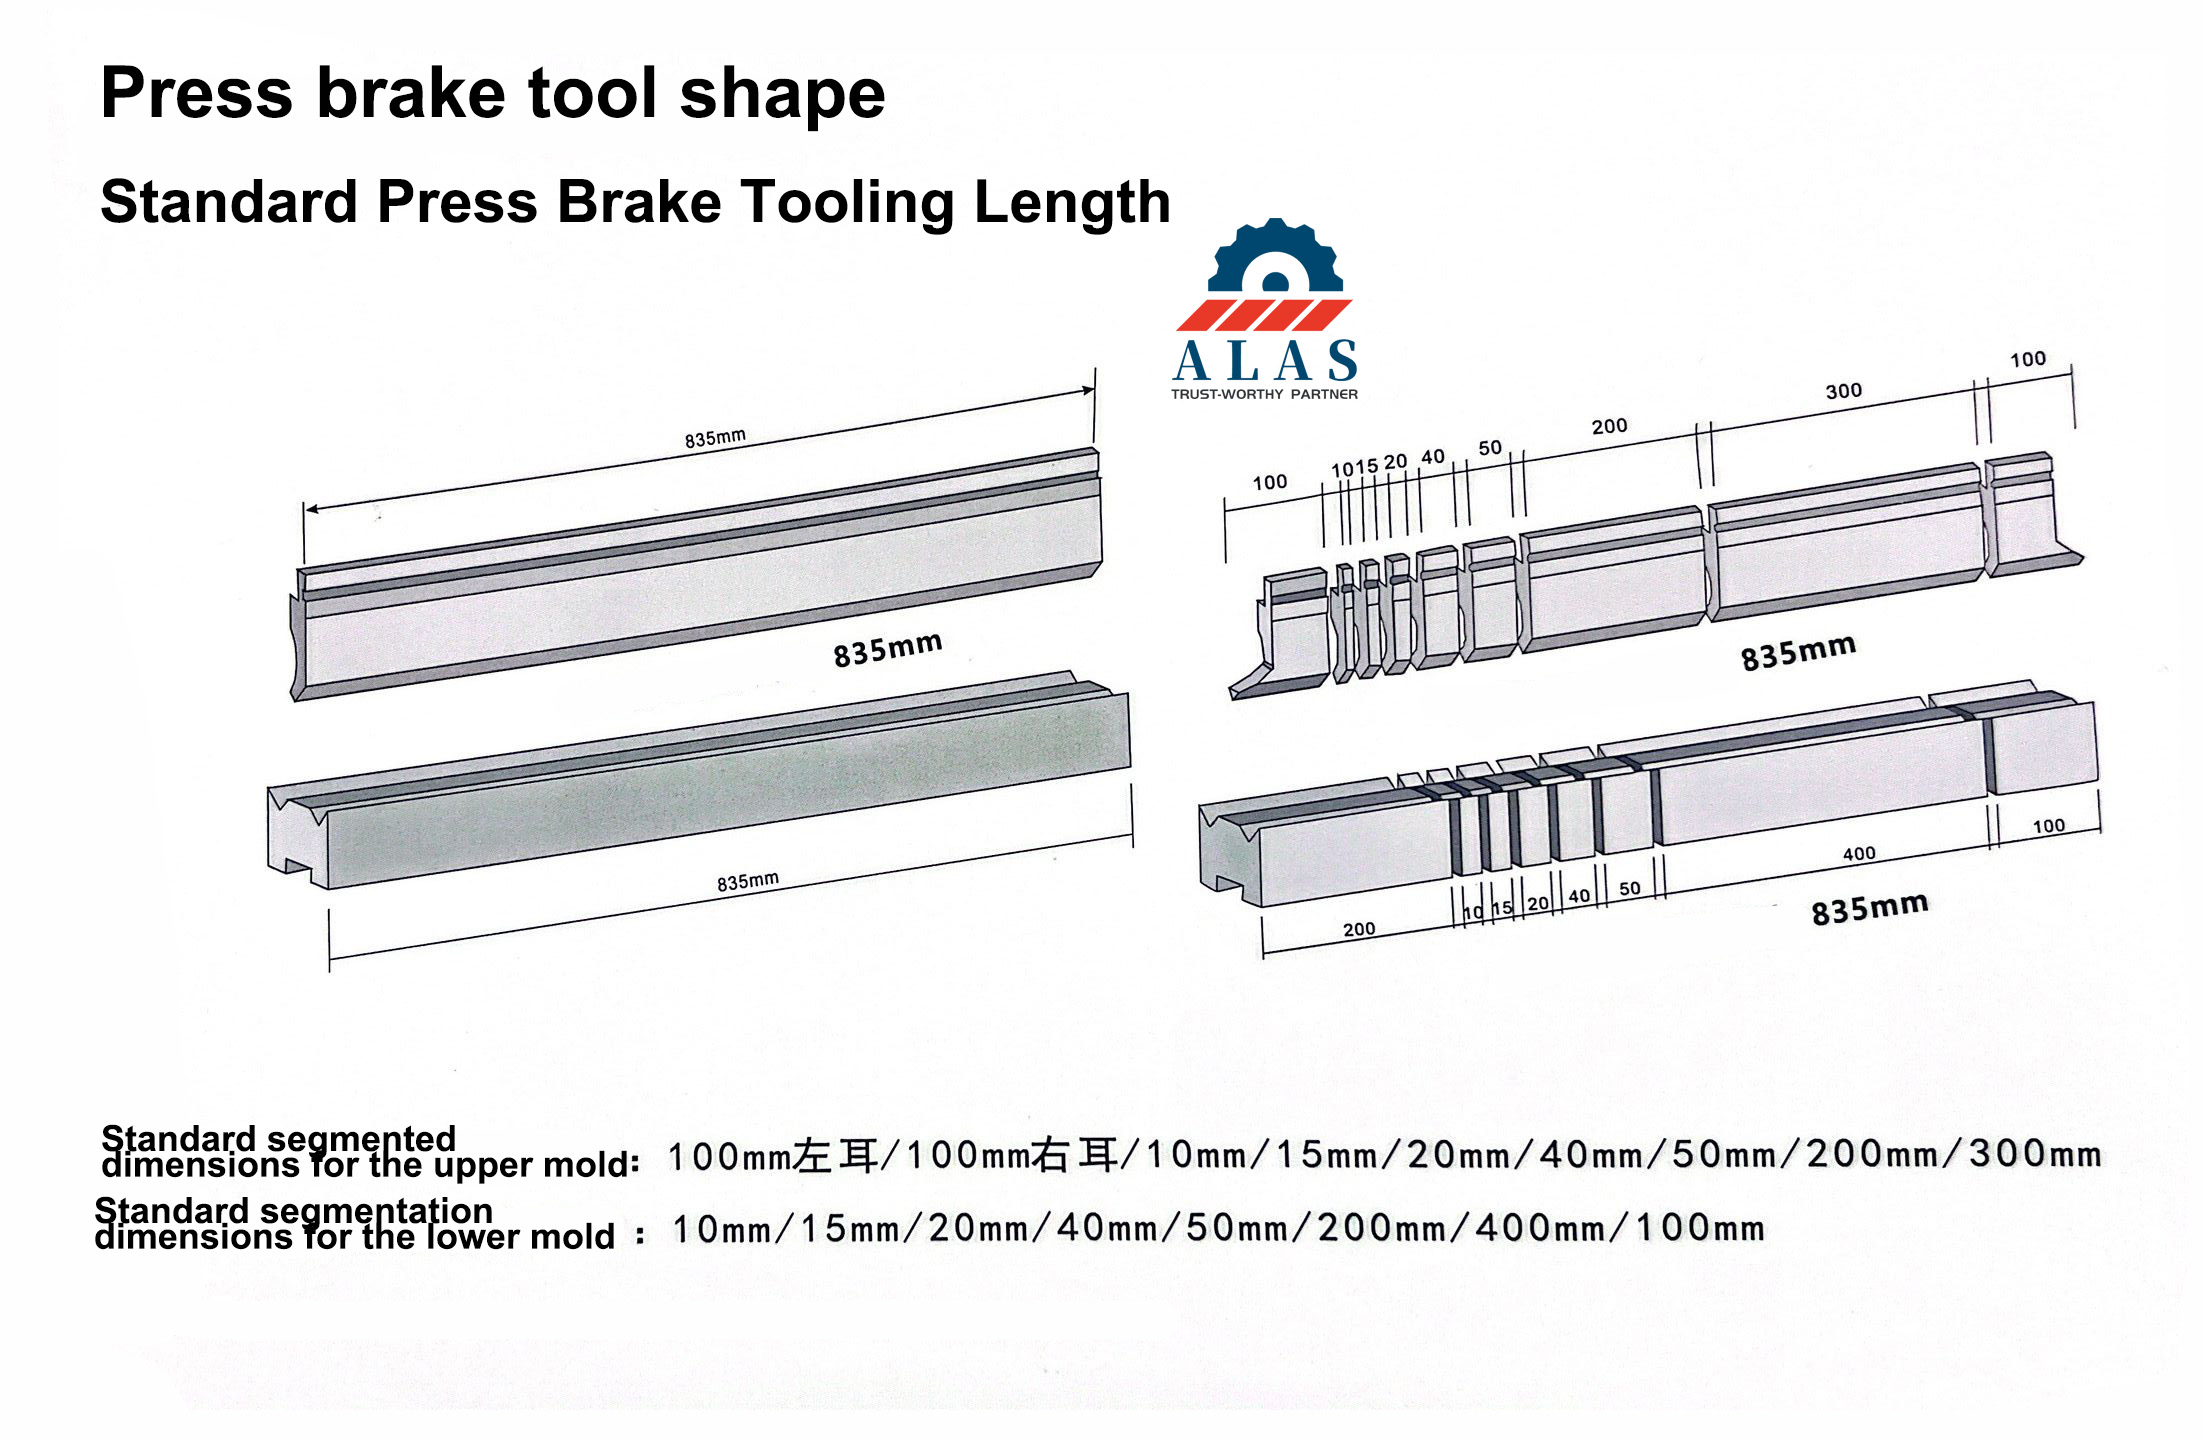
To accommodate varied sheet metal workflows, ALAS manufactures both solid single-piece blocks and precision split segmented kits. Segmented kits are assembled from finely ground matching blocks, ideal for forming closed-contour boxes and multi-sided flanges.
Feature | Full-Length Integral Die | Precision Segmented Die Kit |
|---|---|---|
Standard Lengths | 835 mm, 1000 mm, 2000 mm (Single integral pieces) | Pre-cut fractional blocks: 10, 15, 20, 40, 50, 100, 200, 300 mm |
Primary Target | Long, continuous straight-line sheet metal bending. | Deep box forming, localized partial bends, and closed pans. |
Adjustment Mode | Loosen and rotate the entire solid die block body. | Rearrange or remove split sections to match desired width. |
Storage Footprint | Compact, single-piece rack layout. | Requires sorted, classified toolbox compartment storage. |
Box Bending Tip: For standard deep-pan box production up to 735mm, couple our segmented multi-V lower die with an ALAS gooseneck upper punch to completely eliminate part-collision with side flanges.
Machine Safety Setup: Lower the press brake slide to its baseline position, shut off the hydraulic system, and completely dump all residual line pressure.
Die Cleaning: Thoroughly wipe down the worktable surface. Clean out all scale, metal chips, slag, and old lubricants from the unused V-grooves.
Block Rotation: Manually loosen the lock plates and rotate the die block 90° or 180° until your target V-opening faces directly upward.
Locking & Center Alignment: Securely tighten the clamping bolts. Run a low-pressure test cycle to ensure the upper punch tip aligns perfectly with the center axis of the V-groove.
Scrap Test Bending: Perform a sample bend using identical scrap metal gauge. Verify the final bending angle, stroke depth, and surface finish before batching.
Post-Production Care: Clean the die faces after the shift. Apply a uniform layer of premium light machine oil to provide lasting anti-rust protection during storage.

Tooling Type | Primary Engineering Purpose | Typical Onsite Production Case |
|---|---|---|
Standard V Die | Single-opening right-angle & routine profile forming. | Mass production of identical metal panels. |
Multi-V 4-Way Die | Variable gauge switching, small-batch multi-spec lots. | High-mix general fabrication job shops. |
Radius Tooling | Smooth arc, large-radius fillet, and cylindrical forming. | Decorative sheet facades and structural curves. |
Gooseneck Punch | Deep box channels and deep-return flange clearance. | Complex electrical chassis and double-return covers. |
Hemming / Flattening Tools | Sheet edge folding, pre-bending, and flush flat crimping. | Removal of sharp edge burrs on commercial lockers. |
Onsite Matching Solution: Pairing one standard ALAS 16-50mm 4-way lower die with a single gooseneck upper punch covers roughly 85% of standard metal-forming shop workflows.

The Challenge: A medium-sized metal enclosure factory in Thailand processes over 200 distinct part designs weekly. Materials range constantly between 1.2mm and 4.0mm. Utilizing standalone single-V blocks required 8 to 10 full die changeouts per shift, draining 2 full hours of machine production time daily.
The Solution: The engineering team retrofitted their line with one standardized ALAS 42CrMo 4-Way Multi-V Die Set (V-Openings: 16 / 24 / 35 / 50 mm).
The 3-Month Operation Result:
Setup Efficiency: Single tooling change time plunged from 15 minutes down to just 20 seconds via simple block rotation.
Labor Recovery: Cumulative tool change time fell from 120 minutes down to less than 15 minutes per shift.
Capital Savings: One integrated 4-way die block cost 40% less than procuring four individual standalone lower tools.
Tool Longevity: Zero structural shoulder deformation or micro-cracking observed after 50,000 continuous compression cycles.
A: Yes. A standard acute or universal upper punch tip easily cycles through all four openings. For high-precision parts, ensure your punch tip radius complements your smallest V-groove shoulder to prevent material scoring.
A: Our most popular workshop combination is 16/24/35/50mm. However, we also offer 12/20/30/45mm setups. Custom-tailored layout configurations can be engineered at our manufacturing plant.
A: ALAS 4-way dies are geometrically optimized for 3-point air bending. Bottom bending forces the metal deep into the root under high tonnage, which escalates wear and reduces the longevity of rotatable tooling bases.
A: Absolutely. Simply submit your machine's exact model number or bed dimension print, and our CNC shop will mill a custom base adapter profile to match your factory setup.
Nanjing Alas International Co., Ltd. is a professional industrial tooling manufacturer focused on shear blades, bending dies, shredder blades, and custom wear parts. We offer full application engineering, material selection, setup guidance, and after-sales support to global customers.
Tell us your requirements, and our engineering team will provide professional solutions for blade specification, tool life optimization, and cost-effective production.